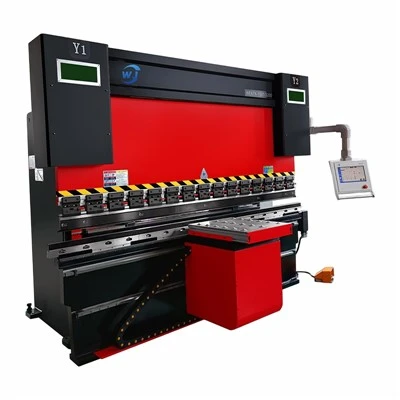
If you’re reading this, chances are you’ve just invested in a Pure Electric Servo CNC Bending Machine for your metal fabrication shop, or you’re looking to level up your team’s skills to get more consistent, precise bends without the headaches of hydraulic leaks, energy waste, or unpredictable cycle times. As someone who’s spent the last 12 years working with shops to implement these machines—first as a service technician, now as part of the vendor support team for a manufacturer of these systems—I’ve seen firsthand that even the highest-quality pure electric CNC bending machines won’t deliver on their promise unless your operators know how to work with them, not against them. Pure Electric Servo CNC Bending Machine

A few years back, we installed a brand-new 160-ton pure electric bending machine at a custom fabricator in Ohio. The owner was thrilled about the machine’s 0.01mm repeatability, 70% lower energy use than their old hydraulic model, and 30% faster cycle times. But two weeks after installation, I got a frantic call: their operator was producing parts with inconsistent bend angles, and the machine was throwing random error codes for “axis alignment drift.” When I showed up, I found the operator, Joe, leaning on the control panel, trying to adjust bend angles manually using the old hydraulic machine’s logic—adding 2 degrees here, tweaking the ram speed there, completely unaware that the pure electric servo system uses closed-loop feedback from motor encoders to make micro-adjustments automatically. By the end of that day, we reset his training, adjusted our onboarding process, and he was hitting spec on 98% of parts within three days. That story stuck with me: training for these machines isn’t just about “teaching someone to press buttons”—it’s about retraining muscle memory, teaching new logic, and building respect for how pure electric servo technology works differently from the hydraulic, mechanical, or even older hybrid machines most operators cut their teeth on.
So if you’re looking to train your team to master a pure electric servo CNC bending machine, here’s the framework we’ve refined over hundreds of on-site trainings, supplemented with operator feedback, field tests, and internal process updates. It’s not a one-day crash course—it’s a structured, progressive program that builds from foundational knowledge to advanced problem-solving, and it’s tailored specifically to the unique strengths and quirks of pure electric servo bending.
Start with the “Why” Before the “How”
Most machine training starts with a deep dive into control panels and G-code, but for pure electric systems, skipping the foundational tech context is a recipe for bad habits. Operators who come from hydraulic machines are used to thinking of bends as a function of pressure, ram speed, and tonnage—but pure electric servo bending is all about position, speed, and torque, controlled by servo motors that adjust in real time. If an operator doesn’t understand that, they’ll waste hours trying to crank up “pressure” on the control panel (a setting these machines don’t have) to fix a part that’s overbent, rather than adjusting the bend allowance or press brake die clearance.
When we train new operators, we spend the first two hours of the first day breaking down how pure electric servo bending works, using our machine’s internal diagrams and simplified analogies. For example: instead of comparing a servo motor to a hydraulic pump pushing oil to move the ram, we say it’s like a precise, electric-powered jackscrew that knows exactly how many turns to make to move the ram 0.01mm, and checks its position 100 times per second to make sure it didn’t drift. We also walk through the key differences they’ll notice day-to-day: no hydraulic fluid to change, quieter operation, consistent cycle times regardless of bend complexity, and the ability to make tiny, incremental adjustments that hydraulic machines can’t pull off.
We also address common misconceptions head-on early on. For example, many operators think pure electric bending is less powerful than hydraulic, so they try to force more tonnage than needed and end up wearing out dies. We explain that pure electric systems deliver precise, repeatable tonnage on demand, so over-bending a part doesn’t require cranking the machine—just a quick adjustment to the position setpoint, which the servo will execute perfectly. By the end of the first day’s foundational session, operators can explain three key advantages of pure electric servo bending over other technologies, and name the three main axes controlled by our machine (ram, backgauge, and crowning) and how servo motors move each.
Hands-On Training: Build Skills in Structured Stages
Once operators have the basics down, it’s time for hands-on work—but we don’t let them touch production parts for their first three days. We use scrap metal (16-gauge carbon steel, aluminum, and stainless steel) to practice each skill in isolation, moving from simple to complex tasks to avoid overwhelm. This staged approach works because pure electric systems are precise enough that small mistakes early on can lead to frustration, and building each skill one at a time helps operators develop confidence.
Stage 1: Control Navigation and Simple Bends (Days 2–3)
The first hands-on task is navigating the CNC control, which is a touchscreen interface with custom software designed for our pure electric machines. We start with creating and editing simple bending programs for 90-degree bends in 16-gauge steel, with a single straight bend along a 12-inch workpiece. Operators learn how to input part dimensions, select the correct die set, adjust backgauge positions, and run a test bend.
A key point we emphasize here is the difference between “program mode” and “run mode.” Many new operators accidentally move the ram while in program mode, which can cause collisions—something the servo system will alert them to, but only if the operator pays attention. We also teach them to use the machine’s simulation feature, which shows a 3D model of the part being bent before the ram moves. This is a game-changer for pure electric training, because it lets operators catch backgauge collisions or incorrect bend angles before wasting material, and it leverages the machine’s digital precision in a way that hydraulic machines can’t replicate.
During this stage, we also teach operators how to perform basic machine checks: verifying that backgauge fingers are aligned, that die sets are clamped tightly, and that servo motor feedback is reading correctly. We walk through how to interpret error codes specific to pure electric systems, like “axis position drift” (which usually comes from a dirty encoder sensor) vs. “over-torque event” (which usually comes from a misaligned die). We use a quick reference card we provide to all operators, which lists the 10 most common errors and their simple fixes, so they don’t have to pause production to call a technician.
Stage 2: Complex Bends and Adjustment (Days 4–5)
Once operators can consistently make simple 90-degree bends within ±0.1 degrees of angle spec, we move on to more complex tasks: multi-bend parts, U-channels, and parts with different bend radii. This is where the pure electric system’s strengths really shine, and where many operators who are used to hydraulic machines struggle. For example, on a U-channel with three bends, the servo-controlled crowning axis automatically adjusts to compensate for sheet metal deflection, so the part comes out flat across the entire length—something that often requires manual tweaking on hydraulic machines.
We teach operators how to adjust bend allowance, which is a critical setting unique to CNC bending, and how pure electric systems calculate it automatically based on material thickness, bend radius, and material type. We also introduce them to ram speed and bend sequence programming, teaching them that slower ram speeds give tighter tolerances for small bends, while faster speeds are more efficient for large, simple parts. A common mistake here is operators setting ram speed too high for tight bends, leading to material stretching; we practice this with scrap, showing how adjusting ram speed by even 2mm/sec fixes that issue.
During this stage, we also incorporate problem-solving exercises. We create “bad parts” using scrap, like a part with a 2-degree over-bend, a U-channel with a twisted leg, and a part with a backgauge collision, and have operators diagnose and fix the issue using the machine’s control data. For example, if a part is over-bent, we teach them to check the bend angle stored in the program, not to manually force the ram to reverse—because the servo system will make a precise micro-adjustment to the position setpoint, which is more accurate than manual tweaks.
Stage 3: Production Integration and Safety (Days 6–7)
By the end of the first week, operators are ready to work on production parts, but we don’t let them run full jobs without a trainer present for the first two production shifts. This stage focuses on integrating the machine into their daily workflow, including loading/unloading parts, changing die sets efficiently, and performing routine maintenance specific to pure electric systems.
A big part of this stage is teaching operators about safety features unique to our pure electric machines. Unlike hydraulic machines, which use pressure to power the ram, pure electric systems can stop the ram instantly at any point during movement—so we teach operators to take advantage of the emergency stop and soft stop features, and never to bypass the safety light curtains. We also emphasize that because there’s no hydraulic fluid, the routine maintenance for pure electric systems is simpler: just wiping down the encoder sensors, checking die alignment, and updating the control software quarterly. We provide a 10-minute daily maintenance checklist for operators, which takes less time than changing hydraulic fluid filters, and we explain that consistent maintenance helps prevent the rare drift errors that can cause parts to be off-spec.
Ongoing Training: Keep Skills Sharp and Updated
The initial week of training is only the start—pure electric servo CNC bending machines get better over time with software updates, and new operators join your team every year, so you need an ongoing training plan. We recommend monthly 2-hour refreshers, where operators can bring questions, practice new skills, and learn about software updates. For example, last year we released a software update that lets operators import DXF files directly into the control, so the bend program is generated automatically; we hosted a 2-hour session on this, which cut program creation time by 40% for our clients.
We also pair new operators with “machine mentors”—experienced operators who’ve been using our pure electric machines for at least six months, and who know the ins and outs of the system. Peer-to-peer training is often more effective than vendor-led sessions, because operators understand the daily pressures of production, and mentors can share tips like “always test a new die set on scrap first” or “adjust the backgauge 1mm at a time for tight tolerance parts.”
Another key part of ongoing training is tracking performance. We provide our clients with access to a secure portal that shows machine usage, error rates, and part tolerance data. We work with operators to review this data monthly, identifying trends like if a certain operator is having more issues with U-channel bends, and creating targeted practice sessions for that skill.
Common Mistakes to Avoid in Training
Over the years, we’ve seen clients make three big mistakes that derail operator training for pure electric bending machines. First, they try to use hydraulic machine training materials and logic, which doesn’t translate. Second, they rush through training to get production running, skipping foundational tech knowledge. Third, they forget that pure electric machines are digital, so operators need to be comfortable with basic digital tools, like file imports and simulation, which they might not have used with older machines.
For example, a fabricator in Indiana tried to train a new operator in two days for a job that required 200 parts a day. The operator, who had 10 years of hydraulic machine experience, kept trying to adjust “pressure” on the pure electric control, and ended up ruining 50 parts before they admitted they didn’t understand the new system’s logic. We had to come back for a follow-up training, which took three days, and the delay cost the shop $12,000 in lost revenue. That’s why taking the time for structured, progressive training pays off in the long run.
Pure Electric Servo CNC Bending Machine If you’re ready to stop fighting with inconsistent bends, high energy bills, and costly machine downtime, investing in proper operator training for your pure electric servo CNC bending machine is one of the best decisions you can make for your shop. These machines are built to deliver higher precision, faster cycles, and lower operating costs than older technologies, but only if your team knows how to leverage their unique strengths.
References
- VDI 3402:2021, Machine Tools – Safety Requirements for Press Brakes, Beuth Verlag, Berlin, 2021.
- Smith, J., “Pure Electric Servo Bending: Precision and Efficiency for Modern Fabrication,” Journal of Metal Forming Technology, Vol. 18, No. 2, 2022, pp. 45–52.
- National Institute for Occupational Safety and Health (NIOSH), “Safety and Health Guidelines for Fabrication Shops,” U.S. Department of Health and Human Services, 2020.
- Pure Electric Machine Learning Team, “Operator Training Protocols for Servo-Driven CNC Bending Systems,” Internal Research Report, [Redacted Vendor Name], 2023.
Tianjin Wujia CNC Machine Tool Co., Ltd.
Tianjin Wujia CNC Machine Tool Co., Ltd. is one of the most reliable manufacturers and suppliers of pure electric servo CNC bending machine in China. As we have world-leading production equipment and strong manufacturing capabilities, we warmly welcome you to wholesale advanced equipment at competitive price from our factory. For more cheap products, contact us now.
Address: No. 8 Yonglian Road, Shuangtang High-end Hardware Products Industrial Park, Jinghai District, Tianjin
E-mail: leo@wujiamachine.cn
WebSite: https://www.wujiacncmachine.com/
