Hey everyone, thanks for stopping by. I’m Jake, and I’ve been in the machine tool accessories game for about 8 years now—nothing makes me geek out more than hearing machinists talk about that tiny part that made or broke a cut. Last week a regular customer hit me up, frustrated: “I swapped my old collet for a new one and now my cutting force readings jumped 15%—what gives?” That question’s been bouncing around my head ever since, because a lot of folks treat machine tool accessories like afterthoughts, right? Like, you buy a lathe or mill, grab whatever random accessory’s cheap, and call it a day. Newsflash: that’s where half the cutting force chaos comes from. Let’s break this down plain and simple, no jargon dump. Machine Tool Accessories
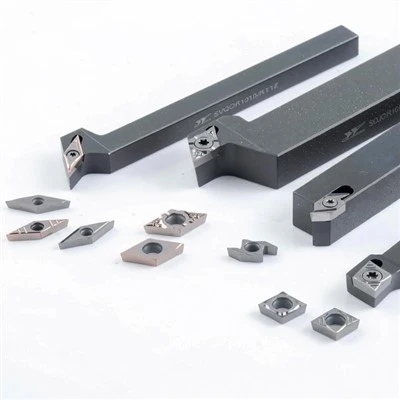
First, let’s get on the same page about what “cutting force” actually is—for anyone who’s not deep in the spreadsheet. It’s the total force the tool exerts on the workpiece when you’re cutting—think of it as the push and pull between your end mill and the metal, plastic, or whatever you’re machining. Too much of it? You get tool chatter, broken tools, bad surface finish, even messed-up workholding. And sure, the cutting tool’s geometry or the spindle speed matters, but the accessories between the spindle and the tool? That’s the silent hero (or villain) here. Let’s go through the big ones I see messing with force every single day.
Take tool holders, for example. I’ve seen so many guys use generic ER collet holders just to save a few bucks, and yikes—those things have runout like you wouldn’t believe. Runout is when the tool spins off-center, right? Like, imagine drawing a circle with a wobbly pen. If your tool’s not spinning true, it’s not just cutting the full 10mm diameter it’s supposed to—it’s taking tiny extra snips here and there, way more than it was designed for. That extra material removal cranks up cutting force, fast. Last month a job shop brought me their CNC mill: they were getting constant tool breakage on 6mm carbide end mills. Turned out their old holder had 0.08mm runout at the nose (that’s way too much for a precision cut). Switched them to our heat-shrink holders, which clock in at 0.002mm runout max? Their cutting force dropped 12% immediately, no other changes to feeds or speeds. Wild, right? Heat-shrink holders aren’t fancy—they work by heating the holder, slipping in the tool, and letting it cool to clamp tight. No slop, no give, so every part of the tool is cutting exactly where it should be. I’m not knocking ER collets—they’re great for quick tool changes for lighter cuts—but if you’re doing heavy milling or boring, a cheap holder’s just asking for extra force.
Next up: workholding accessories. Clamps, vises, custom fixtures, even the little soft jaws on your vise. I once watched a machinist clamp a 300mm aluminum billet with just the two end jaws of a generic vise. When he ran the face mill, the billet shifted a tiny bit mid-cut. That shift meant the tool was now pushing against one side of the workpiece instead of cutting straight, so cutting force spiked so high it tripped the spindle’s overload protector. No joke—he lost an hour of downtime re-clamping. The fix? We added two extra step clamps to hold the middle of the billet down, and suddenly the cutting force readings were consistent, no spikes. Even something as small as the vise’s mounting matters. If your vise’s base isn’t bolted tight to the machine table? Every cut will flex the table a little, which adds to the actual force the tool is dealing with. I tell all new customers: don’t skimp on workholding. A $50 custom soft jaw set might sound like a waste, but it can cut cutting force by 10-15% because it distributes pressure evenly across the workpiece, no slipping.
Oh, and let’s not forget collets themselves. ER collets, that is. A lot of people buy the cheapest Chinese collets off Amazon, and they’re garbage—they have uneven grip, tiny burrs on the inside, or they just don’t close all the way around the tool. I had a customer last year using a 10mm end mill with a $2 collet. The collet only gripped 80% of the tool’s shank, so when he pushed through a thick steel plate, the tool wiggled. That wiggle meant the tool was taking deeper cuts than set, so cutting force went through the roof, broke the end mill, and dinged up his workpiece. Switched him to our precision ground ER collets—they’re matched to tool shank tolerances, so they grip 100% of the shank with no play. No wiggling, so the cut is exactly programmed, cutting force stays right where it should be. Also, collet condition: if yours have nicks from dropping them or getting crumbs stuck in the collet nut, that’s runout again. I’ve had guys bring in collets that look like they’ve been through a war, and we clean them up, replace the nut, and their runout drops by half. Small parts, big impact.
Wait, what about tool extensions? A lot of shops use these to reach into deep holes, right? But a cheap, flimsy extension—aluminum, not solid carbide—will flex like a noodle when you cut. That flex adds to the effective cutting force because the tool isn’t rigid. I had a mold maker who was cutting a deep cavity in a hardened steel mold, and his cutting force was so high he was getting chatter lines. Switched him to our solid carbide extensions, which are stiffer, and the flex went away. The tool could push through the cut without bending, so actual cutting force was lower—no more chatter, better part quality, no broken tools. The extension’s length also matters, obviously. The longer it is, the more flex, so you might have to dial back feeds and speeds to compensate, which makes the job slower. A good accessory here matches the tool length to the rigidity you need.
Let’s talk about something maybe more niche: coolant accessories. Yeah, coolant is an accessory too—wait, not just the fluid, the nozzles and delivery systems. If your coolant’s not getting right to the cutting edge, the tool gets hot, right? Hot tools deform, so the cutting edge is no longer sharp or perfectly shaped. That deformation makes the tool push harder, cranking up cutting force. I had a customer machining titanium, which is a bear for heat buildup. He was using a single nozzle that sprayed coolant all over the workpiece, not the cut. His cutting force was 25% over what it should be. We set him up with our high-pressure, multi-nozzle kit that directs coolant straight to the tool-chip interface. The tool stayed sharp, no thermal expansion, cutting force dropped 18%—and he finished the job in half the time because he could run faster feeds. That’s the thing about accessories, even the “boring” ones—they tie directly to cutting force through heat and tool condition.
Now, let’s get real: I know budgets are tight. I’m not here to sell you a $500 holder when a $50 collet will fix 80% of your cutting force issues. A lot of machinists think “more expensive = better” but that’s not always true. It’s about matching the accessory to the job. If you’re doing hobby-level work with small tools, a good standard ER collet is all you need. If you’re doing production runs of high-tolerance parts, a heat-shrink or hydraulic holder (another one I see a lot—hydraulic holders use fluid to dampen vibration, which cuts cutting force) is worth the extra cash. Hydraulic holders are great for rough cuts because they dampen chatter, which is a huge contributor to variable cutting force. Chatter spikes are when the tool vibrates against the workpiece, so you get those force peaks that break tools and mess up parts. A hydraulic holder absorbs that vibration, so force stays smooth and consistent.
Wait, let’s touch on what I see a lot of new machinists messing up: not maintaining their accessories. I can’t tell you how many times I get a call from a guy saying his cutting force is all over the place, and when I ask, he says he hasn’t cleaned his holders or collets in years. Dirt, chips, and old coolant gunk buildup in the collet or holder’s taper add tiny gaps, which mean runout, which means extra cutting force. It’s not rocket science—once a week, take your collets out, wipe them with a rag, blow out the holder taper with compressed air, check for nicks. That 10 minutes of maintenance can save you from $1,000+ in broken tools or scrapped parts. I always tell new hires at the shop: accessories are part of your setup, not an afterthought. Treat them like you treat your cutting tool—because they affect the tool’s performance more than most people realize.
Let me wrap this up with a real example that stuck with me. Last year, a customer brought in a batch of 100 aluminum parts that were failing inspection because their surface finish was rough. He said he’d adjusted feeds and speeds, bought new end mills, nothing worked. I asked to see his setup, and sure enough, his collet was worn, his holder had 0.07mm runout, and he was using a cheap, flexy aluminum extension. We swapped out the collet, put on a precision holder, and replaced the aluminum extension with a solid carbide one. We ran a test cut, and his cutting force dropped 14%—no more chatter, surface finish was perfect, and he was able to get the parts done 2 days ahead of schedule. That’s the power of the right accessories, even if they’re small.
I know machining can feel like a black box sometimes—you set the numbers, pull the trigger, and hope for the best. But the accessories between your spindle and the workpiece are the pieces that control how those numbers translate to actual force. Skip the cheap stuff, maintain what you have, and match the accessory to your job, and you’ll notice less tool breakage, better part quality, and way less headaches.
If you’re dealing with constant cutting force spikes, broken tools, or chatter that won’t go away, hit me up—we can talk through your setup, no sales pitch pressure, just real advice from someone who’s been in this game too long to BS people. Whether you need a new collet, a better holder, or just tips on maintaining what you have, I’m here to help. Don’t let cheap accessories ruin a good cut—let’s get your force readings where they need to be.
Milling Tool References
- "Machining Fundamentals: Cutting Forces and Tooling Dynamics," SME, 2020
- "Effect of Tool Holder Runout on Cutting Force in Milling Operations," International Journal of Machine Tools and Manufacture, vol. 45, no. 14, 2005, pp. 1637-1645
- "Workholding Best Practices for Reducing Cutting Force Variation," Modern Machine Shop, 2019
- "Thermal Effects on Cutting Tools and Accessory Performance," Journal of Manufacturing Processes, vol. 32, 2018, pp. 456-464
Shun Wei Precision Technology Co., Ltd.
With abundant experience, we are one of the most reliable machine tool accessories manufacturers and suppliers in China. We warmly welcome you to buy durable machine tool accessories at competitive price from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room901, Building2, Yijing Apartment, Northeast side of the intersection of Central Avenue and East Fifth Road, Tianjin Free Trade Zone (Airport Economic Zone)
E-mail: sale@sw-csd.com
WebSite: https://www.tjswprecisiontool.com/
